Leuze: Sensors for Safe Material Flow in SEW-Eurodrive's High-Bay Warehouse
Some time ago, SEW-Eurodrive opened a smart factory for the production of shafts and gear components. A key component of the expansion is a fully automated production buffer warehouse, for which the company relied on Sivaplan’s intralogistics expertise and Leuze’s sensor expertise.
Anyone entering the world of drive technology and drive automation cannot ignore SEW-Eurodrive: The products from this family-owned company based in Baden-Württemberg power nearly everything that moves—from baggage handling systems at airports to package sorters in e-commerce logistics centers to conveyor systems in networked production environments.
SEW-Eurodrive continuously invests in its locations. Most recently, this included Graben-Neudorf, near its corporate headquarters in Bruchsal: Here, the company opened a smart factory for the production of shafts and gear components at the end of 2024. A key component of the expansion is a fully automated production buffer warehouse in the North Hall, where SEW-Eurodrive has relied on Sivaplan’s intralogistics expertise and Leuze’s sensor expertise.
A Systematic Approach to Buffers
The logistics module—a fully automated, single-aisle high-bay warehouse—serves as a production buffer between gear and shaft manufacturing and the hardening shop: “The automated warehouse decouples the machining processes of soft machining, hardening, and hard machining,” explains Michael Schütz, head of the hardening shop at SEW-Eurodrive. “In the hardening shop, the gear components and shafts are treated in special furnaces to make them more resilient, wear-resistant, and durable.”
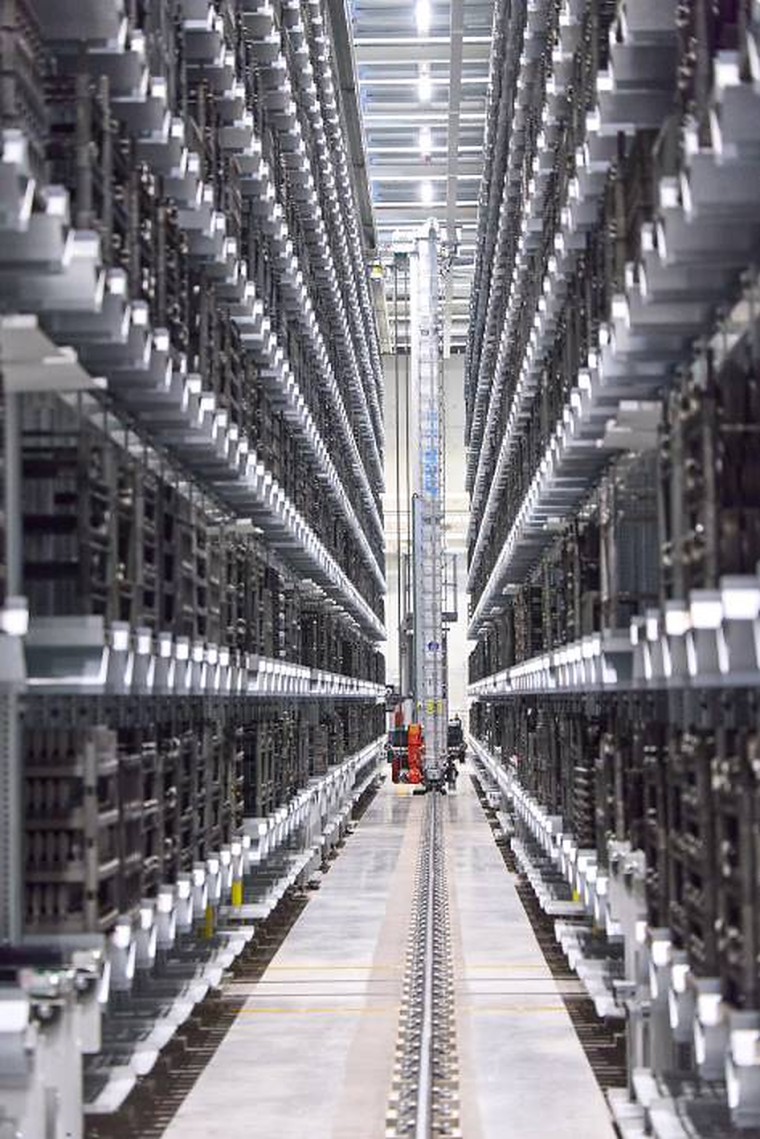
The dimensions of the warehouse, constructed from 70 metric tons of steel, are impressive: Two nine-meter-high racks extend over a length of more than 76 meters and are each five meters wide. They are designed with double-deep storage—meaning that two racks can be stored one behind the other on each side of the rack. In total, the module offers 2,300 storage locations. Between the two racks, two automated storage and retrieval machines (AS/Rs) operate fully automatically along a travel axis. “The SRVs transport the special hardening racks—containing the products—delivered from production and transfer them to the furnace system.
After hardening, the racks containing the shafts and gear components are also returned to storage via the RSVs and dispensed as needed for further processing,” says Christian Langsdorf, Head of Sales at Sivaplan. The total conveyor length is 152 meters. The stacker cranes perform heavy-duty work: a single rack, including the material, weighs up to 510 kilograms.
Green Light for Mobile Robots
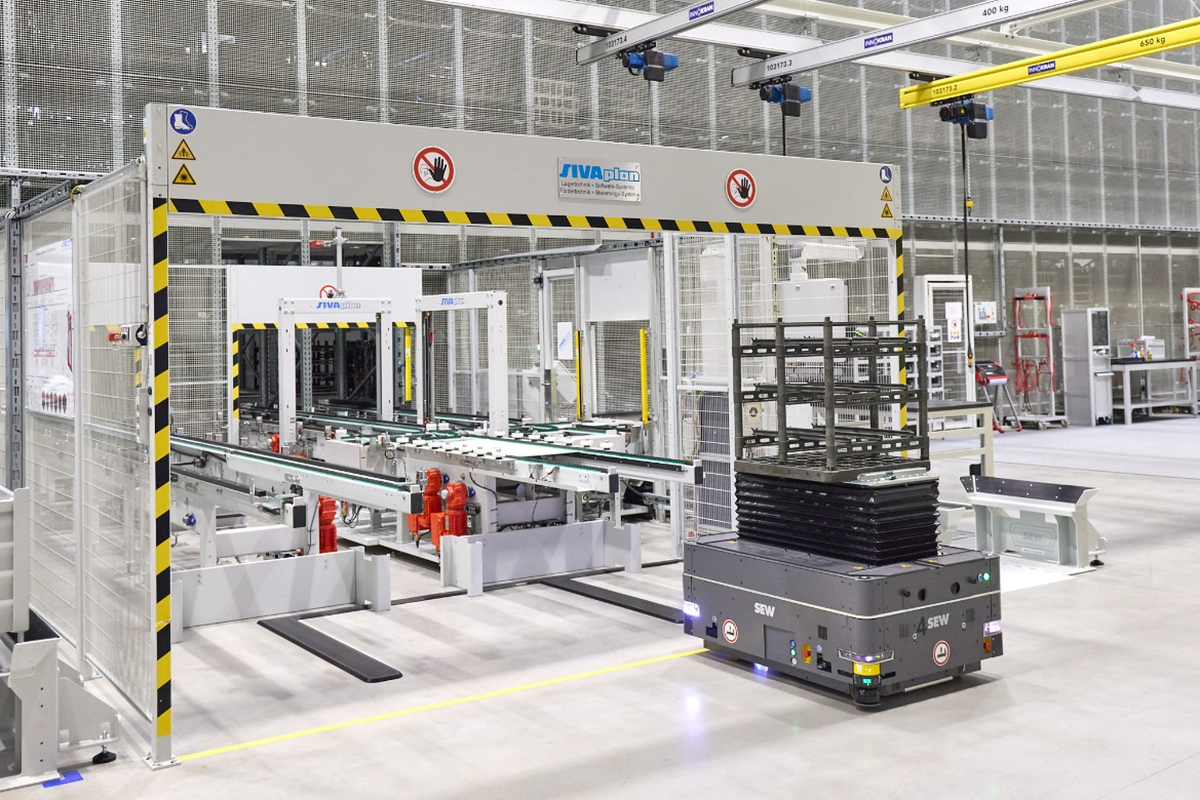
As a specialist in fully automated warehouse technology, Sivaplan implemented the logistics module—including the higher-level control system—on a turnkey basis. As the general contractor, the Troisdorf-based company was also responsible for implementing the higher-level control system in collaboration with Procam Steuerungstechnik. It communicates with and coordinates all subordinate machines, systems, and vehicles.
In addition, the control system handles all processes with the higher-level ERP system (SAP). Sivaplan has thus supplied numerous important core elements that contribute significantly to the efficient and autonomous operation of production. A key component of the warehouse is the sensor technology from Leuze: “Sivaplan’s solutions and Leuze’s sensor expertise complement each other perfectly,” says Christian Langsdorf. “We have been working together in a spirit of trust for many years and are convinced of the reliability and quality of Leuze’s sensor technology. That is why we continue to rely on this partnership time and again for new projects.”
Leuze’s products play a role in numerous process steps, ensuring that everything runs safely and efficiently during the storage and retrieval of the racks. This begins as soon as the goods are delivered: Mobile robots from SEW-Eurodrive automatically transport finished components to the high-bay warehouse.
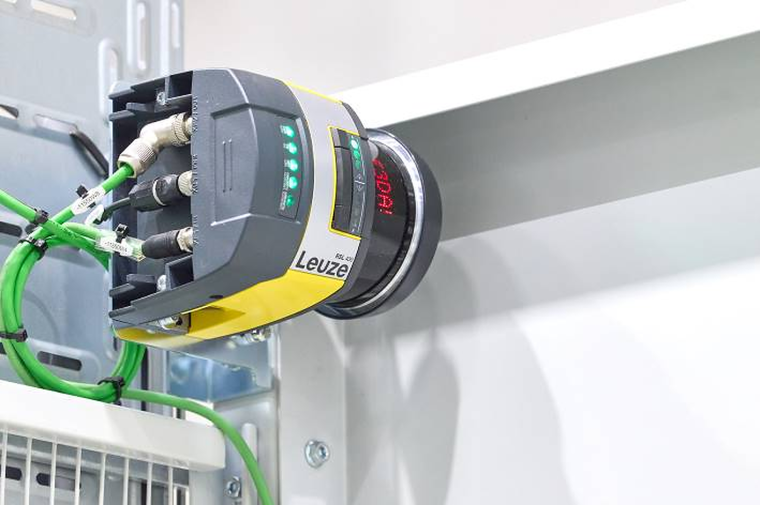
The mobile robots are controlled by the higher-level control system. Above each material transfer station, two Leuze RSL 400 safety laser scanners are installed to reliably secure access to the facility.
“The RSL 400s generate a vertical protective field and grant access once the mobile robot has successfully registered. The mobile robot can then deliver the goods through this opening. Access remains secured on the side of the vehicle,” emphasizes Frank Wüster, Sales Manager at Leuze.
They then pick up the material from production. After a short drive into the hall, they transfer the load via four loading and unloading stations—material transfer stations. As soon as the mobile robot has passed through the open safety field area, the field is reset to its original, closed state. Convenient: Thanks to the integrated Profisafe/Profinet interface, the RSL 400 can be integrated into the safety control system with ease.
In-line contour inspection
After the AGV transfers the loaded rack, it is transported via the conveyor system to a contour inspection station. Leuze HT25C reflective photoelectric sensors detect the racks and control the conveyor system. Once the racks reach the contour inspection station, their outer contours are captured in-line by CML 720i measuring light curtains.
The inspection results are output via the integrated Profinet interface. To control the light curtains, additional Leuze sensors are installed to detect the presence of the racks. One advantage of this setup is that the photoelectric sensors detecting toward the delivery area are designed with a high-visibility vest suppression feature, as Frank Wüster explains: “This prevents false detections caused by people wearing high-visibility vests who are standing in front of the transfer station or walking past it—a practical feature.”
Also part of the sensor system at this station are industrial IP cameras from Leuze: They additionally capture images of the racks. They are installed to the sides and above the contour inspection station.
Safe Loading and Unloading
To ensure that SEW-Eurodrive employees have the ability to manually remove and inspect racks, a manual workstation is integrated into each material transfer station. MLC 530-SPG safety light curtains ensure that the loading and unloading of racks is performed safely at all times.
Of particular note is not only the personal safety protection itself, but also the sensorless muting via the patented Smart Process Gating (SPG): This method enables a compact and space-saving system design. A switching signal provided by the PLC and the interruption of the protective field by the conveyed material serve as triggers for activating the gating function. As a result, no additional muting sensors are required immediately upstream or downstream.
The compact safety light curtains are designed to take up minimal space, can be mounted quickly and easily using various brackets, and are controlled reliably via pin assignment. The installed MLC 530-SPG Type 4 units meet the highest safety requirements according to EN IEC 61496 and achieve Performance Level PL e and SIL 3.
“The racks, along with the workpieces to be hardened, enter the furnaces. They are therefore exposed to extreme thermal conditions. This can cause them to deform over time,” says Hardening Department Manager Michael Schütz. “That’s why, after a certain number of furnace cycles, the racks are automatically routed to this station and remeasured there.”
Reach Your Destination with a Barcode
After the goods destined for the hardening shop have been measured, one of the storage and retrieval machines picks up the rack. Here, too, precise processes are essential to ensure that the goods reach their designated storage location safely and reliably. The stacker cranes are therefore positioned using Leuze FBPS 600i safety barcode positioning systems, which ensure reliable speed monitoring in conjunction with the latest-generation MOVI-C inverters from SEW-Eurodrive.
The FBPS 600i systems enable safe position detection. The position and speed of the RBGs are continuously monitored based on the system’s status. This is particularly necessary because the two RBGs operate on the same rail. In addition, safe position detection is required to reliably secure two pedestrian walkways in the high-bay warehouse. To achieve this, the system switches the safe envelopes of the travel zones. If people cross the aisle, the RBGs are “held in place” and monitored in defined segments so that this can be done safely.
For safe position detection, only one sensor is required with the FBPS 600i safety barcode positioning system. This significantly simplifies integration and makes system setup much easier. Two FBPS 600i units are installed on each stacker crane: one for positioning the lifting axis and the other for the travel axis. The FBPS 600i safe barcode positioning systems can be used flexibly thanks to reading distances ranging from 50 to 170 millimeters from the barcode tape.
With each scan, multiple codes are read; these are processed internally in a redundant manner and then processed with millimeter precision via the dual SSI interface in the safe connection unit of the SEW inverter. “The scan beam is intentionally positioned at an angle. Thanks to the angled path and the movement of the device, each code is scanned at different points. This prevents reading errors caused by local contamination or damage,” says Oliver Gortner, Key Account Manager for Intralogistics at Leuze.
This solution is compact and space-saving and enables precise, safe positioning of the RBGs in accordance with Performance Level e / SIL 3. In addition, the very short error response time of just 10 milliseconds allows for short braking distances and, consequently, higher speeds. In this way, the FBPS 600i plays a crucial role in fully leveraging the high-bay warehouse’s performance—with minimal installation effort and a high level of safety.
Camera-Based, Precise Placement into the Compartment
Leuze sensors also support operations at the automated storage and retrieval system (AS/RS) and in the rack storage areas: Reflective photoelectric sensors detect the presence of the racks. Once an RBG reaches the designated storage location via barcode positioning, fine positioning of the bin begins: The loaded rack must be placed precisely into the designated storage bin.
For this purpose, a camera-based Leuze IPS 200i sensor with an integrated Profinet interface is mounted on each RBG. The small, compact sensor is suitable for positioning tasks at distances ranging from 100 to 600 millimeters. It focuses on a reflector attached to the rack beam. When the marker is within the IPS 200i’s working range, the sensor transmits absolute values to the SEW controller. This enables the automated storage and retrieval system to precisely take over the rack. An efficient solution that eliminates the need for multiple photoelectric sensors.
Conclusion
With its fully automated high-bay warehouse, Sivaplan has implemented a highly complex logistics system that integrates seamlessly into SEW-Eurodrive’s production processes in Graben-Neudorf. Leuze sensor technology plays a key role at nearly all critical points, ensuring fully automated and safe operations.
It ensures reliable safeguarding of material transfer, precise detection and measurement of the racks, and exact positioning of the rack-feeding devices down to the individual storage bin.
SEW-Eurodrive thus benefits from a production buffer warehouse that flexibly supports manufacturing, absorbs peak loads, and—thanks to its modular design—is suitable for future expansions and adaptations.